


Drive in Pallet Racking
Guangzhou JustBest Logistics Equipment Co., Ltd.: Your Professional Drive in Pallet Racking Manufacturer!
Founded in 2015, Guangzhou JustBest Logistics Equipment Co., Ltd. is mainly engaged in R&D, design, manufacturing, installation and after-sales service of warehousing equipment. The company's main products include pallet racking, flow racking, mobile rack, selective pallet racking, shuttle pallet racking, drive in pallet racking, etc.


why choose us
High-quality products
The shelves are all made of high-quality cold-rolled steel and are strictly quality inspected before leaving the factory, ensuring excellent quality.
Rich experience
In the past twenty years, we provide shelf storage services to companies from all walks of life, work closely with them.
Professional team
Our shelf installation service team all over the world can effectively and quickly solve your storage problems.
One-stop solution
We are committed to providing you with one-stop storage solutions from design, production, transportation, installation to after-sales.
High-density storage heavy load
The drive-in pallet is designed to store 6-8 pallets deep, allowing large quantities of heavy inventory to be stored. The structure is made of steel to withstand the heavy load. This is ideal for businesses with similar yet large storage density needs. You can maximize the horizontal and vertical space. This is ideal for business environments where space is at a premium.
Optimize warehouse space
Drive-in pallets utilize the warehouse space better than most other pallet racks. This system optimizes around 70-80% of available space. The rack eliminates the aisles between racks, creating more space for pallet storage.
Adaptable to structure change
Another great advantage of drive-in systems is their adaptability to structure change. The racks are assembled with bolts, making them easy to move and change the structure for upgrade. This is particularly suitable for dynamic warehouse environments where storage needs change over time.


Suitable for storing large quantities of homogenous materials
Drive-in pallets can handle a high volume of identical products. This makes them suitable for industries like food and beverage, manufacturing, and Distribution centers where inventories are common. Products will have a longer shelf life and product batches will be stored and retrieved instead of a single product.
Low maintenance and low assembly costs
The design of the Drive-in racking is straightforward. Installing them is easier compared to other complex pallet racking systems. Maintenance costs are relatively lower than those of many other storage systems because of the strong structure and materials.
Improve safety
Drive-in racking contributes greatly to the safety of your inventory, let alone the rack itself. Its strong construction provides enough support and stability to heavy loads to prevent accidents caused by shifting or collapsing pallets.
Product Parameters
|
Rack type: drive in drive thru racking system (drive-through rack) |
|
|
Dimensions |
|
|
Overall dimensions Total length: 10 meters Total width: 2.5 meters Total height: 9 meters |
Unit dimensions Unit length: 1.2 meters Unit width: 2.5 meters Unit height: 2.5 meters |
|
Layer height Adjustable range: 200mm - 1,200mm |
Depth Rack depth: 1,200mm (6 pallets deep) |
|
Pallet size Applicable to 1200mm x 1000mm standard pallet |
|
|
Material Material of column: Cold-rolled steel plate, thickness 2.0mm Material of crossbeam: Hot-rolled steel plate, thickness 1.5mm Material of other parts: Stainless steel or galvanized steel |
|
|
Carrying capacity Rated load: Maximum load of 1,500kg per layer Maximum load: Maximum load of the entire shelf is 90,000kg |
Structural features Column: C-section, column spacing is 1,200mm Beam: Fixed crossbeam, with anti-falling devices at both ends |
|
Safety device: The shelf is equipped with anti-tilting and anti-falling devices |
|
|
Surface treatment Coating type: Electrostatic spraying Coating thickness: ≥60μm |
Use environment Temperature range: -10°C to +40°C Humidity range: Not more than 80% (non-condensing) |
|
Installation requirements Ground flatness: ≤5mm/2m Installation tools: Wrench, screwdriver, level ruler, etc. |
|
Application of Drive in Pallet Racking
Drive-in racking systems are versatile and find applications across various industries, including:
Food and beverage
Ideal for storing large quantities of bulk items or perishable goods, drive-in racking facilitates efficient inventory management.
Manufacturing
Used to store raw materials and finished products, drive-in racking supports streamlined production processes.
Retail distribution centers
Helps in managing seasonal stock and high-volume items, optimizing the supply chain and improving service levels.
Pharmaceuticals
Ensures safe and organized storage for sensitive products, maintaining compliance with industry regulations.
Packaging, Shipping and Services
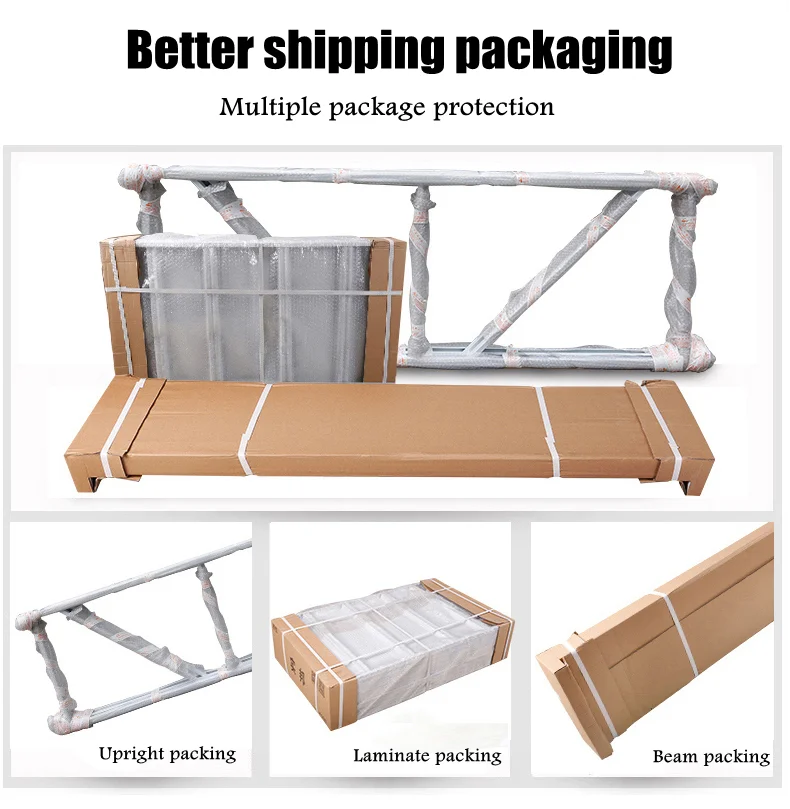


Certifications


FAQ
As one of the most professional drive in pallet racking suppliers in China, we're featured by quality products and low price. Please rest assured to wholesale discount drive in pallet racking in stock here from our factory. Contact us for customized service.
drive in racks warehouse, drive in racking, drive in pallet racking